
Meng Tai Eyewear/Injection Molding
Injection molding
Nineteen presses.
One building.
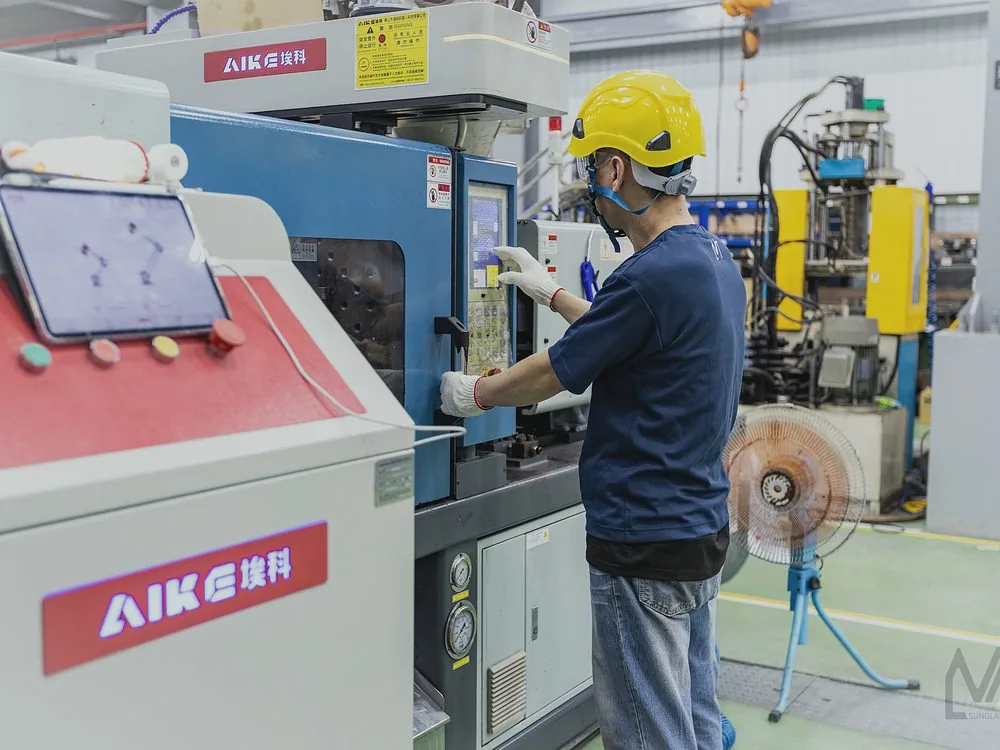
Eleven horizontal injection molding machines for frames and temples, eight vertical ones for over-molding, and a robot cell that takes the gates off. Capacity is more than 130,000 frames a month.
What runs on which machine
The 11 horizontal presses mold the rigid parts — the front, the temples, and the small hardware that goes with them — in PC, TR90, PA66 or PA12.
The 8 vertical presses do the second shot. A part that needs a soft grip goes to them with the TPR molded straight onto it — painted first or not, both run here. That is a separate process with its own page: over-molding.
Degating: hand or machine, and it is priced
Every shot leaves a gate and the gate has to come off. There are two ways to do it here, they cost different amounts, and the choice is yours rather than ours.
By hand is the default. A trimmer cuts the gate with a knife. It is what most orders run, and it is the cheaper of the two.
By machine is an automated cell that cuts the gate and deburrs it. It carries a surcharge, and what the surcharge buys is repeatability: the same cut on the thousandth part as on the first, and the part handled once instead of picked up, turned over and put down again.
We will tell you which one a quotation assumes rather than leaving you to find out from the first shipment.
Tumbling before paint
Molded parts are tumbled before they go anywhere near the spray booth. It takes down the gate witness and evens the surface, and paint laid onto an uneven surface shows every bit of it. This is the step that is quietly skipped when a price looks too good.
Sequence
Six steps, in this order.
The order matters more than the list. Paint goes on before the soft shot, not after — which is why the grip never has to be masked.
On the floor
- Injection
- Tumbling
- Painting
- Over-molding
- Finishing
- Assembly & packing
Frame materials
- PC
- TR90
- TR90 NZZ
- PA66
- PA12
- TPEE / TPR
The tooling is here too
Molds are tried, adjusted and repaired in our own tool room, in the same building as the presses. A problem found on the first shot does not go into a crate — it goes down the corridor. See the tool room.
About the capacity figure
130,000 frames a month is what the floor can run, not a promise about any one order. What a given style actually takes depends on its cycle time, how many cavities its tool has, whether it needs a second shot and how much finishing it carries. We quote against the drawing.
What to send for a quotation
A 2D drawing or 3D file, the material, the annual or per-order quantity, and whether the style exists already or starts from a sketch. If you have a sample part, send that as well — it answers questions a drawing does not.
Send us the drawing.
We will come back on tooling, cycle, material and lead time against the quantity you need.
Request a quotation